
 Call Us Now !
Tel : +86 755 27374946
 Order Online Now !
Email : info@bichengpcb.com
How to Select 1080 Prepreg for Rogers RO3010 and FR-4 Hybrid Lamination?
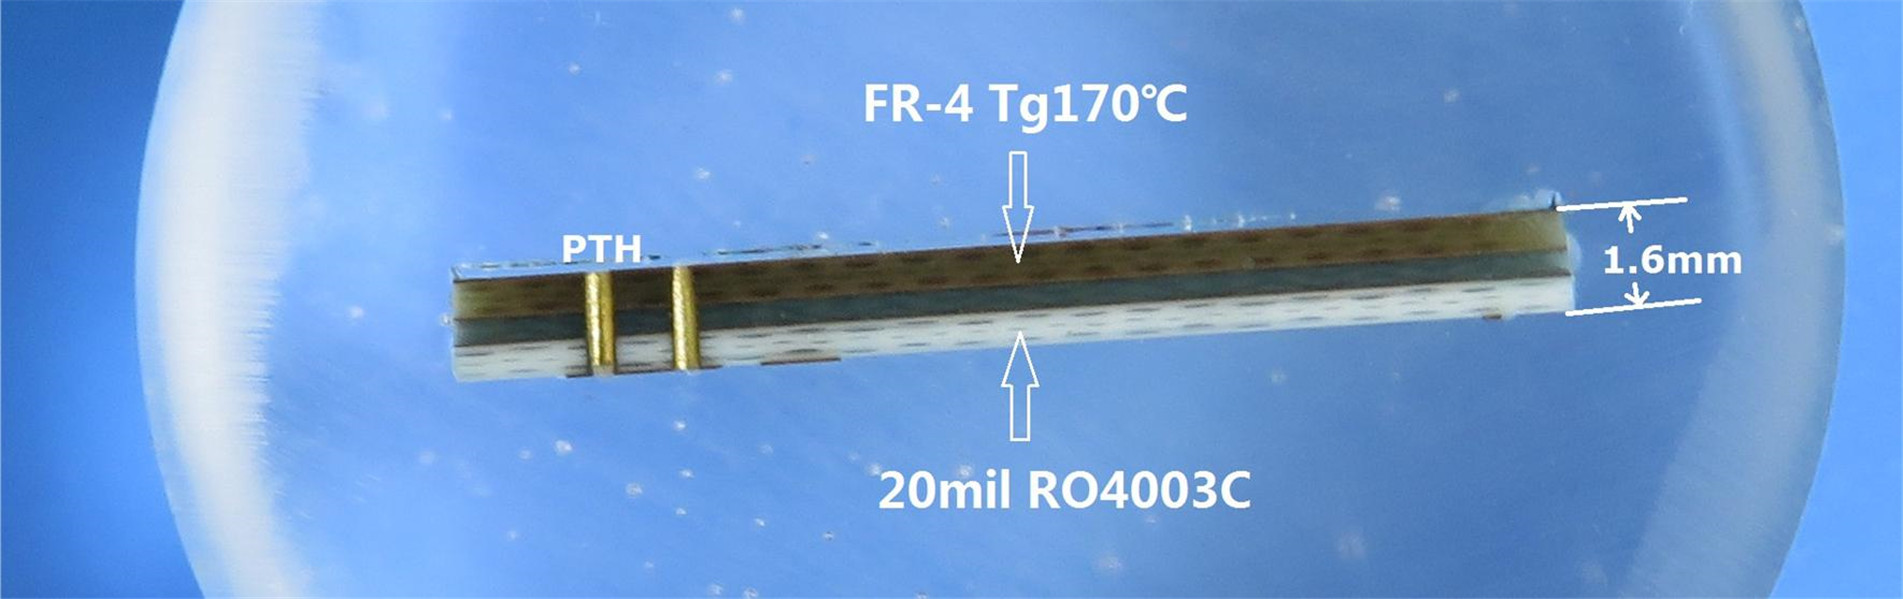
Hybrid multilayer PCBs that pair ceramic-filled PTFE high-frequency laminates such as Rogers RO3010 with conventional FR-4 prepreg have become a standard construction for cost-sensitive RF designs. Place the premium high-Dk material only where RF signals travel, and use economical FR-4 bonding sheets elsewhere. Yet the lamination interface between these two fundamentally different material systems remains one of the most common sources of yield loss and field delamination. This article examines why 1080-style prepreg is the typical bonding-layer choice, what occurs during the press cycle, and the four risk points engineers must control to produce reliable RO3010/FR-4 hybrid boards at volume.
A pure RO3010 multilayer is electrically ideal but materially expensive. RO3010 carries a process dielectric constant of 10.2 ± 0.30 at 10 GHz and a dissipation factor of 0.0022 — properties that come at a significant cost per square meter. By placing RO3010 only on the outer signal layers and using FR-4 prepreg as the inner bonding core, designers retain the high-Dk, low-loss dielectric where RF traces live while reducing total material cost by a meaningful margin.
The 1080 glass style is the most common prepreg selection for this role. Its cured thickness of approximately 0.076 mm (3.0 mil), resin content of roughly 64–68%, and fine-weave structure make it well suited to filling inner-layer copper topography without adding excessive stack height. For a 4-layer board with 1.27 mm RO3010 on both sides, a single 1080 ply provides a thin, compliant bond layer that keeps the finished thickness near 2.8 mm. The table below summarizes the key parameters that make 1080 prepreg the default choice for thin hybrid bonding layers.
|
Parameter |
1080 Prepreg (Typical) |
Relevance to Hybrid Lamination |
|
Glass Fabric Style |
1080 (fine weave) |
Uniform resin distribution; minimal weave-induced Dk variation |
|
Cured Thickness |
≈ 0.076 mm (3.0 mil) |
Thin bond layer; minimal added Z-height |
|
Resin Content |
64 – 68 % |
High fill volume for inner copper topography |
|
Resin Flow |
High (35 – 45 %) |
Good gap filling around traces and via lands |
|
Dk @ 10 GHz |
≈ 3.71 – 3.77 |
Low-Dk bond layer; negligible effect on outer-layer RF |
|
Df @ 10 GHz |
≈ 0.018 – 0.020 |
Thin layer keeps total dielectric contribution low |
|
Standard Roll |
1.26 m × 300 m |
Wide availability; consistent lot-to-lot quality |
Heavier prepreg styles such as 2116 (≈0.12 mm, ≈52% resin) or 7628 (≈0.18 mm, ≈45% resin) carry less resin per unit thickness and are more prone to resin starvation over dense copper. For thin hybrid cores where fill capability matters, 1080 remains the pragmatic default.
During vacuum lamination, the stacked book is heated under pressure. The FR-4 epoxy resin in the prepreg softens around 80–100 °C, flows to fill gaps between copper features, and cross-links as temperature rises toward 180–200 °C. The PTFE matrix in RO3010, by contrast, does not melt or flow — it remains dimensionally stable throughout the cycle. This asymmetry — one material flowing and curing while the other stays rigid — is the root cause of most hybrid lamination defects. The flowing epoxy must wet a non-polar PTFE surface, fill copper topography without trapping air, and cure while constrained by a material that expands at a very different rate. Control of ramp rate, dwell time, pressure, and vacuum determines whether the interface forms a reliable bond or a latent failure that passes electrical test but delaminates in the field.
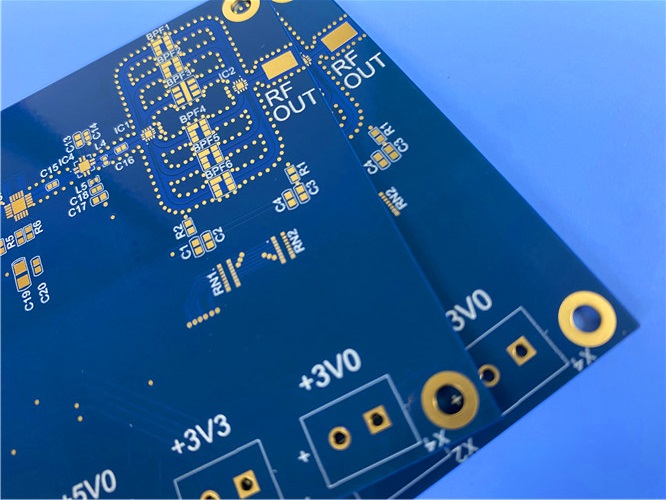
RO3010 has a coefficient of thermal expansion (CTE) of 13 ppm/°C in the X axis, 11 ppm/°C in Y, and 16 ppm/°C in Z, measured from −55 °C to +288 °C per IPC-TM-650 2.4.41. Standard FR-4, by contrast, exhibits a Z-axis CTE of 50–70 ppm/°C above its glass transition temperature (typically 130–180 °C). During lamination cool-down, the FR-4 prepreg contracts far more in the Z direction than the RO3010 cores, creating residual stress at the interface. In asymmetric or thick stacks, this stress manifests as board warpage or bow.
For a 2.8 mm finished board with 1.27 mm RO3010 on both sides, the symmetric arrangement helps balance stress, but copper distribution or resin-flow deviations can still induce camber. Fabricators mitigate this by selecting low-CTE, high-Tg FR-4 prepreg, maintaining symmetric stackups, and controlling cool-down below 3 °C/min through the Tg region.
PTFE has an inherently low surface energy of approximately 18–20 mN/m — the same property that makes it non-stick in cookware also makes it difficult to bond. The RO3010 surface that contacts the FR-4 prepreg must be properly activated to achieve acceptable peel strength. Without surface treatment, the epoxy resin wets the PTFE poorly, and the resulting bond can fail under thermal shock or solder float.
Standard FR-4 inner-layer oxide or brown oxide treatment is not sufficient for PTFE. Fabricators typically use plasma etching (with He/O₂ or N₂/H₂ gas mixtures) or chemical etching to raise the surface energy of RO3010 before lamination. Peel strength at the hybrid interface should be verified through microsection and solder-float testing (260 °C, 10 seconds, IPC-TM-650 2.4.8). A bond that passes initial electrical test but has marginal adhesion can delaminate after multiple lead-free reflow cycles in end-use assembly.
Voids are unfilled spaces between layers, ranging from 10 μm to several millimeters, that form when trapped air, moisture, or contamination prevents resin flow. In hybrid boards, the non-flowing RO3010 surface can trap air at the interface, particularly around via holes and dense copper. Resin starvation occurs when the 1080 prepreg does not carry enough resin to fill inner-layer copper topography, leaving thin spots over trace edges. White spots (measling) appear as localized pale areas where resin has not fully flowed. While 1080's high resin content (64–68%) provides more fill volume than 2116 (≈52%), a single ply may still be insufficient for high copper-density boards. Fabricators should calculate resin demand from copper area and trace height, and verify fill through first-article cross-section analysis.
Both RO3010 and FR-4 prepreg absorb moisture from the atmosphere, though through different mechanisms. RO3010 has a low nominal moisture absorption of 0.05% (D48/50 per IPC-TM-650 2.6.2.1), but the ceramic-filler-to-PTFE interface can trap trace moisture. FR-4 epoxy prepreg is hygroscopic and can absorb more than 0.5% water if stored outside controlled conditions. During lamination, moisture above approximately 0.1% vaporizes at temperatures above 100 °C, generating steam pressure that creates voids, delamination, or popcorn-style cracking at the hybrid interface.
Standard practice requires pre-baking RO3010 cores for 2–4 hours at 150 °C before lamination, storing prepreg below 50% RH with strict FIFO rotation. Vacuum below 5 torr during press further reduces outgassing by removing evolved vapor before it is trapped at the interface.
The following table consolidates the four risk points, their root causes, and the primary mitigation actions for quick reference on the production floor.
|
Risk Point |
Root Cause |
Primary Mitigation |
|
Warpage / Bow |
Z-CTE mismatch (RO3010 16 vs FR-4 50–70 ppm/°C) |
Low-CTE high-Tg prepreg; symmetric stackup; <3 °C/min cool-down |
|
Interfacial Delamination |
Low PTFE surface energy (18–20 mN/m); poor wetting |
Plasma or chemical activation of RO3010; solder-float peel verification |
|
Voids / Resin Starvation |
Trapped air; insufficient resin fill over copper |
Calculate resin demand; vacuum <5 torr; first-article cross-section |
|
Outgassing / Popcorning |
Moisture >0.1% vaporizing at lamination temp |
Pre-bake RO3010 2–4 h @150 °C; controlled humidity storage; FIFO |
Based on production experience with RO3010/FR-4 hybrid boards, the following practices consistently improve yield and long-term reliability:
· Specify low-CTE, high-Tg FR-4 1080 prepreg with resin content verified by incoming lot inspection, not just datasheet nominal values.
· Maintain symmetric stackups with balanced copper distribution on both sides of the neutral axis to minimize residual stress.
· Pre-bake RO3010 cores for 2–4 hours at 150 °C and store FR-4 prepreg below 50% RH with strict FIFO rotation.
· Apply plasma or chemical surface activation to RO3010 bonding surfaces; do not rely on standard brown-oxide treatment alone.
· Use vacuum lamination with 2–4 °C/min ramp, cure at 180–200 °C, and cool-down below 3 °C/min through Tg.
· Perform first-article cross-section and solder-float validation on every new stackup or material lot, verifying peel strength at the hybrid interface specifically.
Hybrid lamination of Rogers RO3010 with FR-4 1080 prepreg is a proven and cost-effective construction for high-frequency PCBs, but it is not a drop-in process. The CTE mismatch between RO3010 (Z-CTE 16 ppm/°C) and FR-4 (Z-CTE 50–70 ppm/°C above Tg), the PTFE adhesion challenge posed by its 18–20 mN/m surface energy, the void and resin-fill risk inherent to a non-flowing high-Dk core, and the moisture sensitivity of both material systems require deliberate process control at every step. By understanding these four risk points and applying the mitigation practices outlined above, fabricators can achieve reliable bonds and consistent yield — and designers can specify hybrid RO3010/FR-4 constructions with confidence.
Bicheng PCB specializes in high-frequency and hybrid multilayer PCB fabrication, including Rogers RO3000/RO4000-series, Taconic, and custom hybrid stackups. Contact our engineering team for stackup review and fabrication feasibility analysis.
Categories
New Blog
Tags
 6-11C Shidai Jingyuan, Fuyong, Baoan, Shenzhen, Guangdong, China 518103


For inquiries about our products or pricelist, please leave to us and we will be in touch within 24 hours.
© Copyright: 2026 Shenzhen Bicheng Electronics Technology Co., Ltd.. All Rights Reserved.

IPv6 network supported


